WORLD electronics offers a complete line of electronic circuit board manufacturing and assembly services, as well as advanced manufacturing services. Our commitment to quality and service is second to no supplier.
Learn MoreOur team of engineers assists you in the development of new designs to optimize quality manufacturability (DFM) and testability, resulting in cost minimization and reduced product development time.
Learn MoreOur flexible manufacturing floor layout and highly trained staff allow for Quick Set-up and Tear Down of small volume prototype runs. This combination grants our customers the benefit of turning new designs quickly and accurately.
Learn MoreWORLD electronics is dedicated to quality. This quality is what underpins our commitment to thorough testing. Our engineers can develop a set of tests that ensure reliability and high performance in all products.
Learn MoreSupply chain management has crossed over from being a narrow management function to being a key operational function.
Learn MoreThe 2026 Top Types of Vacuum Furnace Heat Treatment reflect a market shaped by cleaner surfaces, tighter tolerances, and repeatable metallurgy. Vacuum carburizing, vacuum hardening, solution treatment, annealing, and brazing serve different material demands. Each method changes how components respond under load, temperature, and wear.
David Pye, a recognized heat-treatment author and specialist, states, “The atmosphere is part of the heat-treatment process.” This principle remains highly practical. In a vacuum furnace, pressure, gas purity, heating rate, and cooling speed directly influence the final structure. A stainless-steel part may leave the chamber bright and clean. A tool-steel die may require high-pressure gas quenching for sufficient hardness. Small fixture changes can still create uneven cooling.
Not every cycle behaves perfectly.
Experienced engineers examine more than hardness numbers. They review thermocouple placement, load spacing, chamber leakage, vacuum records, and distortion after cooling. Metallographic inspection can reveal retained austenite, grain growth, or incomplete transformation. These details support reliable decisions and stronger process validation.
This guide compares leading Vacuum Furnace Heat Treatment types for 2026. It also considers applications, material compatibility, operating advantages, limitations, and quality-control needs. Some recommendations may appear obvious. They are not always obvious in production. Furnace size, part geometry, alloy chemistry, and cooling capacity can overturn a convenient choice. That uncertainty deserves attention. Reliable treatment begins with measured evidence, not assumptions.
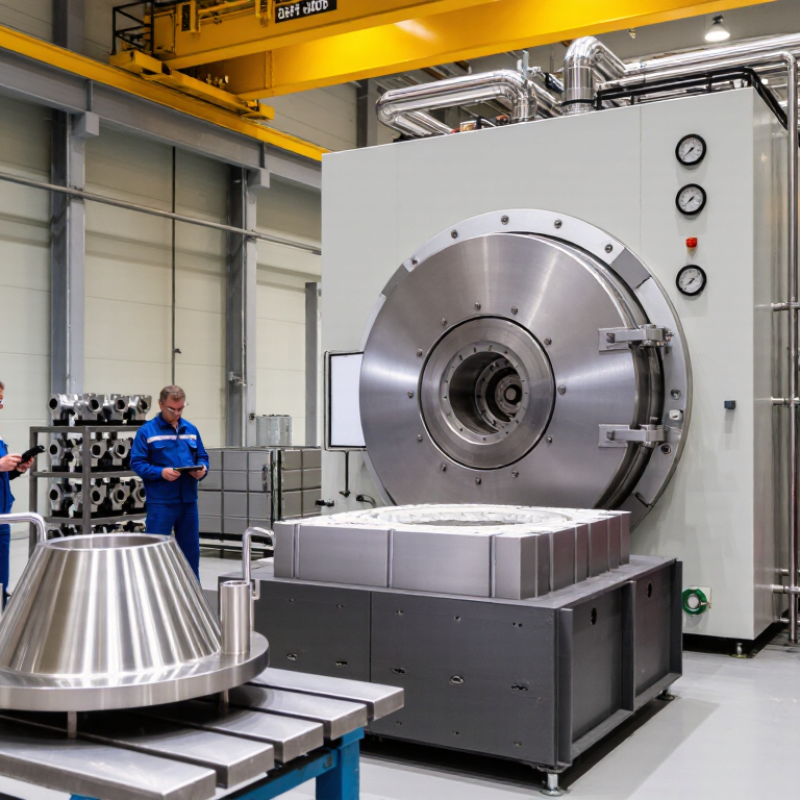
2026 Top Types of Vacuum Furnace Heat Treatment
Vacuum furnaces process metals inside controlled environments, commonly from 10⁻³ to 10⁻⁶ mbar. This pressure range removes most oxygen, moisture, and surface contaminants before heating. Vacuum hardening is widely used for tool steels and precision components. Annealing reduces internal stress and improves machinability. Solution treatment supports selected stainless steels and nickel alloys. Brazing also benefits from clean, oxide-limited surfaces. Each process needs its own temperature, holding time, and cooling method.
In practical operation, pressure stability matters as much as the final vacuum level. A clean chamber, dry insulation, and correctly placed workload reduce contamination. Operators should monitor thermocouples, residual gas behavior, and quench pressure. Gas quenching can cool parts with less distortion than liquid methods. However, thick sections may cool unevenly. The result can disappoint. I have seen excellent hardness values paired with unexpected dimensional changes. That is why load geometry and support design deserve careful review.
Tips: Verify the leak rate before production. Use clean, compatible fixtures. Avoid overloading the hot zone. Record pressure and temperature together, not separately. Compare hardness at several locations after treatment. A low pressure reading does not guarantee clean processing. Residual oil, trapped moisture, or poor pump performance can still affect the surface. Review the cycle when results drift. Small adjustments often reveal larger process weaknesses.
Vacuum annealing softens metal and improves machinability without leaving scale on the surface. Controlled heating reduces internal differences in structure. A typical cycle uses a gradual ramp, a measured soak, and slow cooling. Temperature uniformity matters, especially for thick tools and complex parts. Keep records.
Hardening raises strength by forming a harder microstructure after heating and rapid quenching. The correct quench rate depends on the alloy, section thickness, and required hardness. Gas pressure, cooling speed, and part spacing can change the final result. Small errors matter. Distortion remains possible, even in a clean vacuum environment.
Tempering follows hardening and reduces excessive brittleness. It also adjusts hardness, toughness, and dimensional stability for actual service conditions. Many components need more than one tempering cycle.
Stress relief uses lower temperatures to reduce machining or welding stresses. It can protect tight tolerances before final grinding.
A perfect recipe rarely exists. Load size, surface condition, and furnace calibration can shift the outcome. Experienced technicians compare hardness readings, dimensional checks, and fracture behavior before revising a cycle. They also question unexpected results instead of hiding them.
Vacuum brazing and sintering often run above 900°C, where cleanliness and thermal control become critical. A typical brazing cycle includes pump-down, staged heating, a short soak, filler-metal flow, and controlled cooling. Common brazing temperatures range from 900°C to 1,200°C, depending on alloy chemistry and joint design. Powder-metal sintering may require 1,100°C to 1,400°C, with vacuum levels often selected between 10⁻² and 10⁻⁴ mbar. These are working ranges, not universal rules.
The U.S. Department of Energy’s Industrial Decarbonization Roadmap reports that process heating represents about 51% of industrial energy use. This makes ramp rate, load density, and cooling efficiency important cost factors. In practice, uneven packing can create temperature differences across a large batch. A bright surface does not always prove a sound braze. Metallographic checks and leak testing still matter. Some published cycle charts look precise, yet real furnace behavior can drift after maintenance or repeated loading.
Tips: Verify thermocouple position near the coldest load area. Check residual oxygen, moisture, and furnace leak rate before production. Record pressure and temperature together. Review the cycle after every unusual discoloration, distortion, or incomplete joint. The MPIF Powder Metallurgy industry data also shows that material selection and process consistency strongly influence part performance, so shorter cycles should not be accepted without validation.
2026 Top Types of Vacuum Furnace Heat Treatment
Material choice should guide every vacuum furnace cycle. Tool steel commonly needs vacuum hardening, followed by controlled gas quenching and tempering. This reduces oxidation on cutting edges and limits distortion in thin punches. A bright surface is useful, but hardness must still match the working load.
Stainless steel often benefits from vacuum solution annealing. The process can improve corrosion resistance and reduce carbide-related weaknesses when temperature, holding time, and cooling are properly controlled. Titanium requires special care because oxygen pickup can create a brittle alpha case. High-purity vacuum conditions and rapid inert-gas cooling are essential. Nickel alloys may require solution treatment, aging, or both. Their response depends strongly on alloy chemistry and component thickness.
Tips: Record furnace pressure, load spacing, thermocouple readings, and cooling pressure for every batch. Place thick and thin parts carefully; they rarely cool at the same rate. A recipe copied from another alloy can fail. I have seen acceptable hardness hide poor toughness after rushed tempering. Review test results, inspect the surface, and adjust one variable at a time. No cycle is universally correct.
The chart shows representative industrial temperature windows for common vacuum-furnace heat-treatment processes. Tool steels are typically hardened at high austenitizing temperatures, stainless steels undergo solution treatment at approximately 1,000–1,150°C, titanium alloys are commonly annealed at lower temperatures, and nickel alloys generally require high-temperature solution treatment. Actual settings depend on alloy grade, section thickness, atmosphere, and required mechanical properties.
Vacuum furnace heat treatment is judged by more than temperature settings. Stable production depends on how evenly the load actually heats. A well-qualified furnace can maintain temperature uniformity within ±5°C across the working zone. This figure matters when treating tool steels, aerospace alloys, or precision components. Small temperature differences can change hardness, distortion, and dimensional stability.
Load testing should use calibrated sensors placed near corners, the center, and dense part sections. Empty-chamber results are not enough. Fixtures, baskets, and part spacing can redirect heat. In one practical check, a tightly packed load showed slower heating near its center. The furnace passed without a load, but the production cycle needed adjustment. That result was inconvenient, yet useful.
Gas quenching between 6 and 20 bar gives operators a wider cooling range. Lower pressure can reduce distortion in delicate parts. Higher pressure removes heat faster from thick or demanding loads. Cooling performance depends on gas flow, nozzle design, load geometry, and material thickness. Pressure alone is not a cooling guarantee. Operators should record pressure curves, gas purity, cooling time, and part hardness after each qualification trial. Calibration drift is easy to overlook. A monthly review may still miss a sudden sensor fault. Independent temperature surveys and documented maintenance therefore remain essential for dependable furnace performance.
| Heat Treatment Type | Typical Temperature Range | Primary Process Purpose | Atmosphere / Vacuum Level | Typical Gas Quench Pressure | Typical Temperature Uniformity | Common Materials and Applications |
|---|---|---|---|---|---|---|
| Vacuum Hardening | 950–1,250°C | Austenitizing followed by rapid cooling to increase hardness and wear resistance. | High vacuum, commonly below 10−2 mbar before backfilling with inert gas. | 6–20 bar nitrogen or argon | Up to ±5°C in the qualified working zone | Tool steels, die steels, molds, punches, cutting tools and precision components. |
| Vacuum Tempering | 150–700°C | Reduces quench stresses and adjusts hardness, toughness and dimensional stability. | Vacuum or high-purity inert gas, typically near atmospheric pressure during heating. | Usually not required; controlled gas cooling may use 1–6 bar | Up to ±5°C in the working zone | Hardened steels, tool components, gears and parts requiring controlled final hardness. |
| Vacuum Annealing | 600–1,100°C | Softens material, relieves residual stress and improves machinability or ductility. | Vacuum or inert gas; low oxygen potential minimizes scaling and oxidation. | Controlled cooling, commonly 1–6 bar inert gas | Up to ±5°C in the qualified zone | Stainless steels, alloy steels, nickel alloys, titanium alloys and precision parts. |
| Solution Treatment | 950–1,200°C | Dissolves precipitates or secondary phases before rapid cooling and subsequent aging. | Vacuum, partial-pressure inert gas or high-purity argon. | 6–20 bar for selected alloys and load geometries | Up to ±5°C in the working zone | Nickel-based superalloys, stainless steels, titanium alloys and aerospace components. |
| Vacuum Aging / Precipitation Hardening | 450–850°C | Develops strength and hardness through controlled precipitation reactions. | Vacuum or inert gas to prevent oxidation and surface discoloration. | Natural or controlled gas cooling; commonly 1–6 bar | Up to ±5°C in the qualified working zone | Maraging steels, precipitation-hardening stainless steels, aluminum and nickel alloys. |
| Vacuum Stress Relieving | 500–750°C | Reduces residual stresses caused by welding, machining, forming or additive manufacturing. | Vacuum or inert gas with controlled heating and cooling rates. | Typically no high-pressure quench; 1–3 bar may be used for cooling control | Up to ±5°C in the working zone | Welded assemblies, machined parts, additive-manufactured metal components and fixtures. |
| Vacuum Brazing | 600–1,200°C | Joins compatible components using a filler metal without flux contamination. | High vacuum, often below 10−3 mbar during the brazing cycle. | Controlled cooling or low-pressure inert gas; commonly 1–6 bar | Typically ±5°C or better for filler-metal control | Heat exchangers, carbide tools, stainless assemblies, medical components and aerospace structures. |
| Vacuum Sintering | 1,100–1,500°C | Densifies compacted powders and develops controlled microstructure and mechanical properties. | Vacuum, hydrogen-free inert gas or controlled partial pressure depending on powder system. | Usually controlled cooling; 1–6 bar inert gas when rapid cooling is required | Up to ±5°C in the qualified hot zone | Cemented carbides, powder metallurgy steels, magnetic materials and technical ceramics. |
| Vacuum Carburizing | 850–1,050°C | Introduces carbon into the surface to improve fatigue strength, hardness and wear resistance. | Low-pressure carburizing using hydrocarbon gas pulses under vacuum conditions. | 6–20 bar nitrogen or equivalent inert gas for quenching | Up to ±5°C in the working zone | Gears, shafts, bearings, transmission parts and other low-carbon alloy steel components. |