WORLD electronics offers a complete line of electronic circuit board manufacturing and assembly services, as well as advanced manufacturing services. Our commitment to quality and service is second to no supplier.
Learn MoreOur team of engineers assists you in the development of new designs to optimize quality manufacturability (DFM) and testability, resulting in cost minimization and reduced product development time.
Learn MoreOur flexible manufacturing floor layout and highly trained staff allow for Quick Set-up and Tear Down of small volume prototype runs. This combination grants our customers the benefit of turning new designs quickly and accurately.
Learn MoreWORLD electronics is dedicated to quality. This quality is what underpins our commitment to thorough testing. Our engineers can develop a set of tests that ensure reliability and high performance in all products.
Learn MoreSupply chain management has crossed over from being a narrow management function to being a key operational function.
Learn MoreChoosing among China’s top Pipe Ring Bending Machine manufacturers requires more than comparing prices or polished product photos. A reliable supplier should demonstrate practical experience with steel rings, stainless profiles, aluminum sections, and custom production requirements. Buyers should examine bending diameter, material thickness, roller design, hydraulic capacity, control systems, and repeatability. Small details matter. A clean control cabinet matters.
W. Edwards Deming, a respected manufacturing quality expert, stated, “Quality comes not from inspection, but from the improvement of the production process.” This principle applies directly to Pipe Ring Bending Machine purchasing. A capable manufacturer should show how it controls design, machining, assembly, testing, and after-sales service. Factory videos can help, but documented test results are stronger evidence. Customer references are stronger still.
This guide will introduce leading Chinese manufacturers and explain how their strengths may differ. Some focus on standard machines. Others build customized systems for demanding profiles and larger ring diameters. Their export experience, technical support, spare-parts availability, and operator training also deserve attention. Certification alone is not enough.
The comparison will not pretend to be perfect. Manufacturer rankings can change as products, teams, and service networks develop. That is a weakness worth recognizing. Buyers should request sample bending tests before placing a serious order. Watch the finished ring closely. Check its roundness, surface marks, weld alignment, and springback. The best choice is not always the cheapest machine. It is the supplier that can repeatedly meet your actual production needs.
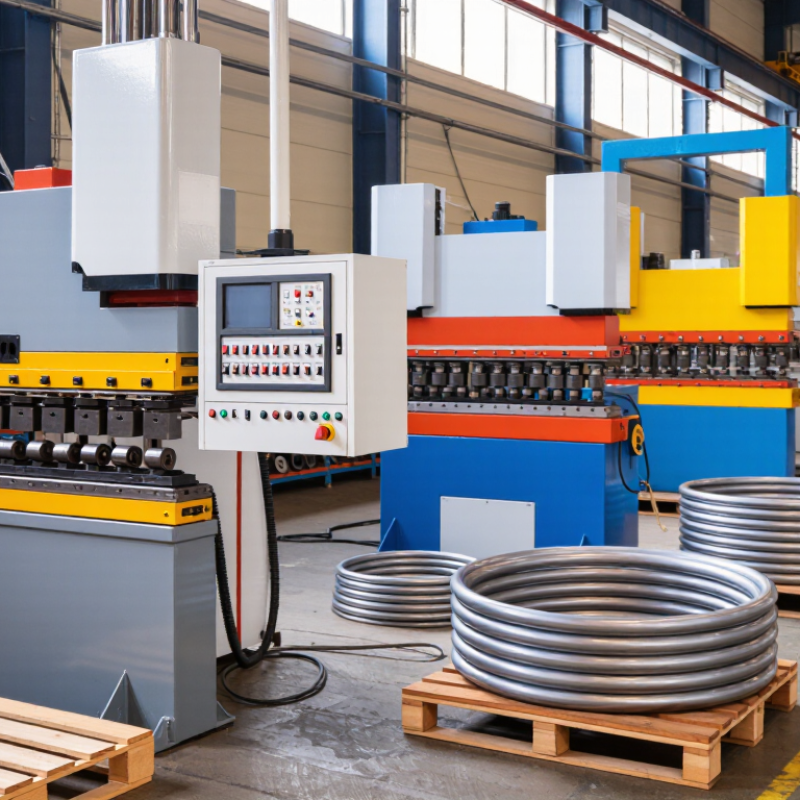
A pipe ring bending machine is industrial equipment that curves straight pipe into a circular or arc-shaped form. It uses controlled pressure, rollers, or forming dies to shape metal without cutting it. The finished pipe may become a tank ring, structural frame, handrail, or curved support.
In a typical workshop, an operator places the pipe between forming rollers and adjusts the spacing gradually. Hydraulic force then pushes the material through repeated passes. This slower process helps reduce flattening, wrinkles, and surface marks. It also gives better control over the final diameter. Small errors matter. A difference of only a few millimeters can affect assembly.
Machine suitability depends on pipe diameter, wall thickness, material, and required bending radius. Carbon steel, stainless steel, and aluminum react differently under pressure. A reliable machine should offer stable roller movement, readable controls, emergency stopping, and repeatable settings. Practical testing is essential, because catalog capacity may not reflect real production conditions. Inspectors should check weld quality, alignment, lubrication points, and the accuracy of sample rings. Even experienced operators can misjudge springback, especially with thick or high-strength pipe. That weakness should be measured and corrected through trial bending, not hidden.
China Top Pipe Ring Bending Machine Manufacturers?
How Pipe Ring Bending Machines Work
Pipe ring bending machines shape straight tubes into accurate circles, arcs, or custom rings. The tube passes between forming rollers while a driven roller applies steady pressure. Each roller controls movement, radius, and alignment. Some machines use three rollers for general work, while others add adjustable guides for tighter tolerances.
The operator enters the required diameter and tube size, then sets the roller spacing. A hydraulic or electric system moves the forming roller gradually. The tube bends through repeated passes instead of one sudden stroke. This reduces surface damage and helps maintain a smooth profile. Thick-wall tubing may need higher force, slower feeding, and stronger support. Thin tubing often requires careful alignment to prevent flattening.
Springback remains a practical challenge. Metal tries to recover slightly after pressure is removed. Not every bend is perfect. Skilled operators usually compensate by bending a little beyond the target radius. They also inspect the first ring with calipers, templates, or a measuring table. Small errors can grow around a full circle. In my view, machine specifications alone are not enough when comparing Chinese manufacturers. Control stability, tooling quality, service training, and repeatability deserve equal attention. A clean test bend reveals more than a polished brochure. Mistakes still happen, especially when material grades vary. That is why documented settings and patient adjustments matter.
| Evaluation Dimension | Machine Type or Feature | Typical Technical Data | How It Works | Practical Application and Selection Notes |
|---|---|---|---|---|
| Bending Principle | Three-roll ring bending | Suitable for circular and spiral forming; commonly used for medium and large pipe diameters. | Three powered or adjustable rolls apply progressive force while the pipe passes through the roll gap. The workpiece is gradually formed into a ring rather than bent in one stroke. | Offers continuous forming and good control of ring diameter. It is often selected when the required ring size is larger than the available die size. |
| Bending Principle | Rotary-draw bending | Uses a fixed-radius tooling set consisting of a bend die, clamp die, pressure die and often a mandrel. | The pipe is clamped to a rotating bend die and pulled around the die along a controlled centerline radius. | Provides accurate bend angles and repeatability. It is suitable for smaller rings, tight radii and applications where dimensional consistency is important. |
| Machine Configuration | Hydraulic pipe ring bender | Hydraulic cylinders provide the forming force; operating pressure and capacity depend on the machine design. | Hydraulic pressure moves rolls, dies or clamping components to deform the pipe progressively. | Delivers high forming force and is suitable for carbon steel, stainless steel and other heavy-wall tubing. Regular inspection of hoses, seals and hydraulic oil is required. |
| Machine Configuration | CNC-controlled ring bending machine | Programmable feed length, bending angle, roll position and forming sequence; some systems support recipe storage. | Servo or digitally controlled axes coordinate feeding, rotation and bending movements according to a programmed profile. | Recommended for repeated production, multi-step profiles and applications requiring reduced operator variation. |
| Workpiece Range | Round pipe and tube | Common production ranges extend from small tubing to large structural pipe, depending on roll size, motor power and wall thickness. | The rolls or tooling contact the outside diameter and apply bending moments until the material reaches the target curvature. | Confirm outside diameter, wall thickness, material grade, minimum bend radius and target ring diameter before choosing a machine. |
| Workpiece Range | Square and rectangular tube | Requires compatible rolls, guides and tooling; corner deformation can be greater than with round pipe. | The section is supported and progressively formed while the tooling controls the orientation of the profile. | Useful for frames, architectural structures and guardrails. Internal support or special tooling may be needed to limit flattening and corner distortion. |
| Material Compatibility | Carbon steel | Generally offers good formability and is widely processed on standard heavy-duty equipment. | The material is plastically deformed beyond its elastic limit while the rolls or die maintain the required curvature. | Springback should be considered, especially with high-strength grades. Test bending is recommended when the material specification changes. |
| Material Compatibility | Stainless steel and aluminum | Can be processed with suitable tooling, surface protection and force settings. | The machine applies controlled forming pressure while reducing surface scratching and excessive localized deformation. | Use clean tooling and appropriate lubrication where permitted. Aluminum usually requires careful control because it is more sensitive to surface damage and cracking. |
| Dimensional Control | Springback compensation | Actual compensation depends on material strength, temper, wall thickness, bend radius and forming method. | After load removal, the pipe partially returns toward its original shape. The machine therefore bends slightly beyond the nominal target. | Compensation is normally established through trial pieces, measurement and stored production settings rather than by relying on one universal value. |
| Quality Indicators | Ovality and wall-thickness change | Control limits should be defined by the drawing, applicable standard or customer specification. | Material flows during bending; the outside of the bend tends to stretch, while the inside tends to compress. | Use proper support, suitable tooling and gradual forming to reduce flattening, wrinkling and excessive thinning. |
| Production Efficiency | Automatic feeding and positioning | May include powered feeding, length stops, encoders and programmable positioning. | The system feeds the pipe to a defined position and coordinates the next bending operation without repeated manual measurement. | Improves cycle consistency and reduces setup time in batch production. It is less critical for occasional, low-volume work. |
| Tooling | Interchangeable rolls and dies | Tool dimensions must match pipe outside diameter, profile geometry and target radius. | Tooling transfers force to the correct contact points and guides the pipe during forming. | Ask for tooling changeover time, available diameter ranges and replacement-part availability when comparing machine configurations. |
| Safety | Guarding and emergency stop system | Important features include guards around pinch points, emergency-stop controls and clearly defined operating procedures. | Safety systems limit access to moving rolls, rotating tooling and the pipe path during machine operation. | Operators should receive training and keep hands, clothing and tools away from pinch points. Lockout procedures are required during maintenance. |
| Inspection | Dimensional verification | Typical checks include ring diameter, bend angle, ovality, end alignment and visible surface condition. | Measurements are compared with the engineering drawing or production tolerance after forming and, when necessary, after springback stabilization. | Calipers, templates, radius gauges, height gauges or coordinate measurement equipment may be selected according to the required accuracy. |
| Selection Criteria | Capacity matching | Machine selection should be based on maximum outside diameter, wall thickness, material strength, minimum radius and ring size. | The required forming moment is determined by the pipe section and material resistance, while the tooling determines achievable geometry. | Published capacity ranges are not universal. Compare the complete technical specification and request a sample bend using the actual pipe material. |
China’s leading pipe ring bending machine manufacturers compete through control accuracy, tooling flexibility, and production stability. The World Steel Association’s World Steel in Figures 2024 reports that China produced about 1.02 billion tonnes of crude steel in 2023. That scale supports a deep supply network for tubes, motors, controls, and replacement parts. Strong manufacturers usually offer CNC systems, programmable bending sequences, and servo-driven feeding. These features reduce manual adjustment and improve repeatability between batches.
The best machines also manage different diameters and wall thicknesses with interchangeable tooling. Hydraulic assistance helps form heavy sections, while variable-speed control reduces surface damage. Digital alarms, overload protection, and guarded work zones show stronger engineering discipline. The ISO Survey 2023 places China among the world’s largest holders of ISO 9001 certificates. However, certification alone does not prove machine quality. Buyers should inspect calibration records, weld quality, test videos, and actual customer acceptance data. A polished brochure is not evidence.
Tips: Ask for a sample bend using your real pipe grade. Check ovality, springback, cycle time, and final radius. Request a written tolerance range. Also examine software language, spare-part availability, and operator training. It is not flawless. Some suppliers still emphasize maximum diameter instead of long-term accuracy. That deserves careful questioning before purchase.
China has many pipe ring bending machine manufacturers serving construction, furniture, automotive, and fabrication workshops. Reliable suppliers usually offer machines for round, square, and rectangular tubing. Their production lines should include frame welding, hydraulic assembly, electrical testing, and trial bending. Ask for photographs of these processes, not only polished catalog images.
A capable manufacturer explains bending radius, pipe wall thickness, tooling materials, and machine capacity clearly. During evaluation, request a sample test using your actual tube. Check the finished ring for flattening, wrinkles, cracks, and dimensional deviation. Digital controls can improve repeatability, but software quality depends on proper calibration.
A strong supplier provides operating instructions, spare-part lists, and responsive technical support. Some factories look impressive online yet provide vague answers. That is worth questioning.
Tips: Compare at least three manufacturers. Request a video of a real bending test. Confirm voltage, tooling size, delivery terms, inspection procedures, and warranty coverage. Ask whether technicians can help with installation and operator training. Do not choose only by price. A lower quote may exclude essential dies, sensors, or replacement parts. Also, review the supplier’s export experience and quality records carefully. Details can be missed. Even experienced buyers should recheck drawings before production, because one incorrect radius can make an entire batch unusable.
Choosing a Chinese pipe ring bending machine manufacturer requires more than comparing prices. Ask for factory videos, equipment photos, and recent production records. A reliable supplier should explain bending capacity, tube diameter, wall thickness, minimum radius, and material compatibility clearly. Vague answers deserve caution.
Request a sample test using your actual pipe. Check the finished ring for roundness, surface marks, weld distortion, and dimensional accuracy. Ask how operators adjust rollers and control springback. Experienced engineers should provide practical recommendations, not only catalog specifications. Inspect the machine’s frame, hydraulic system, electrical cabinet, and safety guards. Quality details matter.
Request drawings before production. Confirm the motor rating, spare parts list, delivery schedule, warranty terms, and remote support. Independent inspection can verify assembly quality before shipment. A manufacturer with documented quality procedures is easier to trust. Still, certificates alone prove little. I have seen impressive paperwork hide weak after-sales communication. That risk should be discussed openly.
Compare the total cost, including tooling, packing, installation, training, and future maintenance. Ask for references from similar applications, but verify them carefully. A dependable manufacturer accepts reasonable questions and records technical changes in writing. Good communication is not a bonus. It protects your investment.